Sponsored article
What Really Determines Edge Quality After Mechanical Sheet Metal Deburring?
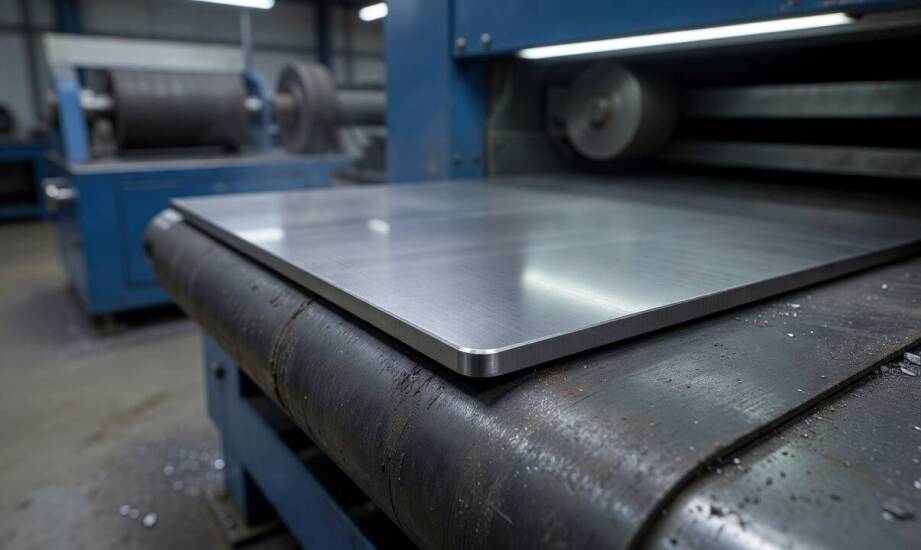
In an automated production line, the same cutting machine can process sheets using an identical program and the same nominal material specifications. Yet after passing through the finishing system, one batch may leave the line with evenly rounded edges and a clean surface, while another still shows sharp burrs or inconsistent material removal.
This difference demonstrates that the final edge quality achieved through mechanical processing depends on multiple overlapping technological factors. Modern automotive, machinery and aerospace industries impose strict requirements on component finishing. Every sharp edge left on a housing or structural component can become a potential corrosion point, reduce coating adhesion and complicate robotic welding processes.
Manual defect removal with angle grinders is slow, inconsistent and potentially harmful to operator health. Understanding the physics of burr formation and the mechanics of their removal in pass-through systems is essential for designing a stable and repeatable manufacturing process.
How Cutting Technology and Metal Alloys Affect Tool Selection
The physical structure of a burr determines both the required tool aggressiveness and the pressure settings within a finishing machine.
Burrs produced by modern fibre laser cutting are typically very thin, hard and razor-sharp. They require precise abrasive contact in order to remove the protrusion without damaging the surface of the workpiece.
Plasma cutting and oxy-fuel cutting leave a thicker buildup in the form of vitrified slag, creating significantly greater resistance during mechanical processing. Punching operations generate yet another defect profile, characterised by edge deformation, material rollover and microcracking. The severity of these imperfections depends largely on the clearance between the punch and die.
Thick plasma-cut parts generally require harder abrasive rollers and higher initial pressure values to achieve effective deburring.
Different alloy compositions also require different processing approaches. Soft aluminium can be easily scratched and thermally deformed through excessive friction. Stainless steel, on the other hand, has a tendency to work-harden, requiring abrasive materials with suitable grain hardness. Such materials also demand controlled cooling to prevent overheating of sensitive surfaces.
Carbon steel is more tolerant of aggressive machining operations and generally offers a wider processing window. Effective sheet metal deburring must take these material differences into account. The same belt pressure will not produce identical results on soft aluminium alloys and hard stainless steel components.
The machine's operating environment is another important factor in process design. Dry processing is generally less expensive and easier to maintain, but it generates significant amounts of airborne dust. Modern dry-processing equipment therefore incorporates multi-stage filtration and spark-separation systems.
Wet processing provides rapid cooling of the workpiece, extends abrasive life and enables safer alternating processing of aluminium and carbon steel components. The use of coolant in wet processing requires regular filtration maintenance and continuous monitoring of fluid condition and pH levels.
Working Head Architecture and Kinematic Parameters
Production volume and the target edge radius determine the required number of machining heads and the movement characteristics of abrasive materials.
In advanced serial manufacturing, machines equipped with three or four independent workstations are becoming the standard. The first section, typically using a wide abrasive belt, is responsible for aggressive removal of the primary burr. Subsequent stations often utilise planetary heads or rotating blocks to perform precise edge rounding from multiple angles using flexible flap brushes.
The final modules are used for surface finishing and for removing oxide residues from the edges.
Smaller fabrication shops often use compact two-head machines, although more complex geometries may require multiple passes through the machine.
The selection of abrasive grain size directly affects cutting efficiency. Abrasives ranging from grit 40 to 80 are highly effective for removing thick slag deposits left by plasma cutting. Belts and brushes within the 120 to 180 grit range are used for fine edge profiling after laser cutting and for creating the desired visual finish.
The process should always progress from aggressive burr removal to gentle edge rounding, protecting flexible brushes from damage caused by hardened metal projections.
Operator-controlled kinematic parameters are equally important for maintaining consistency across an entire production batch. Particular attention should be paid to pressure settings and conveyor speed.
Excessive transport speed significantly reduces the contact time between abrasive grains and the workpiece edge, leaving partially processed areas. Insufficient pressure may cause the abrasive belt to glide over hard oxide layers without removing them effectively.
Excessive pressure can lead to overheating, geometric distortion of the workpiece and premature wear of consumables.
Industrial machine manufacturers increasingly integrate independent control systems into their equipment. Solutions offered by Madora allow operators to calibrate the pressure applied by each workstation directly from the control panel. This architecture enables manufacturers to process different material batches without lengthy mechanical retooling procedures.
Interpreting Edge Defects and Calibrating the System
Visual and tactile inspection immediately after processing remains one of the fastest methods of verifying machine performance.
Sharp burrs remaining on the underside of a cut part clearly indicate incorrect process parameters. Common causes include insufficient roller pressure, excessive conveyor speed or the use of abrasives with a grain size that is too fine for the application.
When burrs bend over instead of breaking away, the grinding roller may be equipped with an excessively soft rubber backing. Conversely, if the edge profile appears properly rounded but deep grinding scratches are visible on the flat surface, the machine is likely applying excessive pressure to a thin metal sheet.
Variations in finishing quality across the working width of the machine create serious production challenges.
Uneven material removal on opposite sides of the table is often an indicator of asymmetric wear in one of the working heads. This commonly occurs when narrow workpieces are consistently processed on only one side of the conveyor, leading to uneven brush wear over time.
Another warning sign is the appearance of dark heat discolouration on steel surfaces. In most cases, this indicates that the abrasive material has become worn out. Instead of efficiently cutting material, the belt generates friction and heat.
The presence of untouched black oxide layers on carbon steel cut with oxy-fuel technology suggests that the cleaning blocks are not reaching the edge deeply enough.
Continuous and informed analysis of visible defects allows experienced operators to distinguish between cutting-machine errors and wear-related issues within the deburring system itself. Correct diagnosis enables rapid adjustment of machine settings, belt tension or station pressure before hundreds of parts from the next production batch are affected.
You might be interested
The Role of Mushroom Diversity in Wholesale Offerings for Culinary Creativity
GDPR Accountability in Technology Companies: Where the Real Role of the DPO Begins
Can clergy wear a zucchetto hat of any color?